At Andy Marine, we believe that practical manufacturing knowledge is one of the most valuable assets built over time.
Inside our workshop, there are engineers, production specialists, and experienced technicians who have spent years working with stainless steel marine hardware — from material selection and casting processes to finishing and quality control.
Many of these insights are learned through daily production experience: understanding why a component fails, how different materials perform in marine environments, and what details truly matter when developing reliable hardware.
However, this practical knowledge is often shared only within the workshop and rarely reaches customers who are making sourcing and engineering decisions.
ENGINEER TALKS is our effort to organize these conversations and share the manufacturing experience behind marine hardware.
Through this series, we discuss materials, production processes, design considerations, and real-world lessons from the perspective of a marine hardware manufacturer.
Today's ENGINEER TALKS Ep.22 is presented by Engineer Zhang, written by me the editor.
1. Two Coils of Chain, One Stamp: Why "10 mm" Is Not Yet an Answer
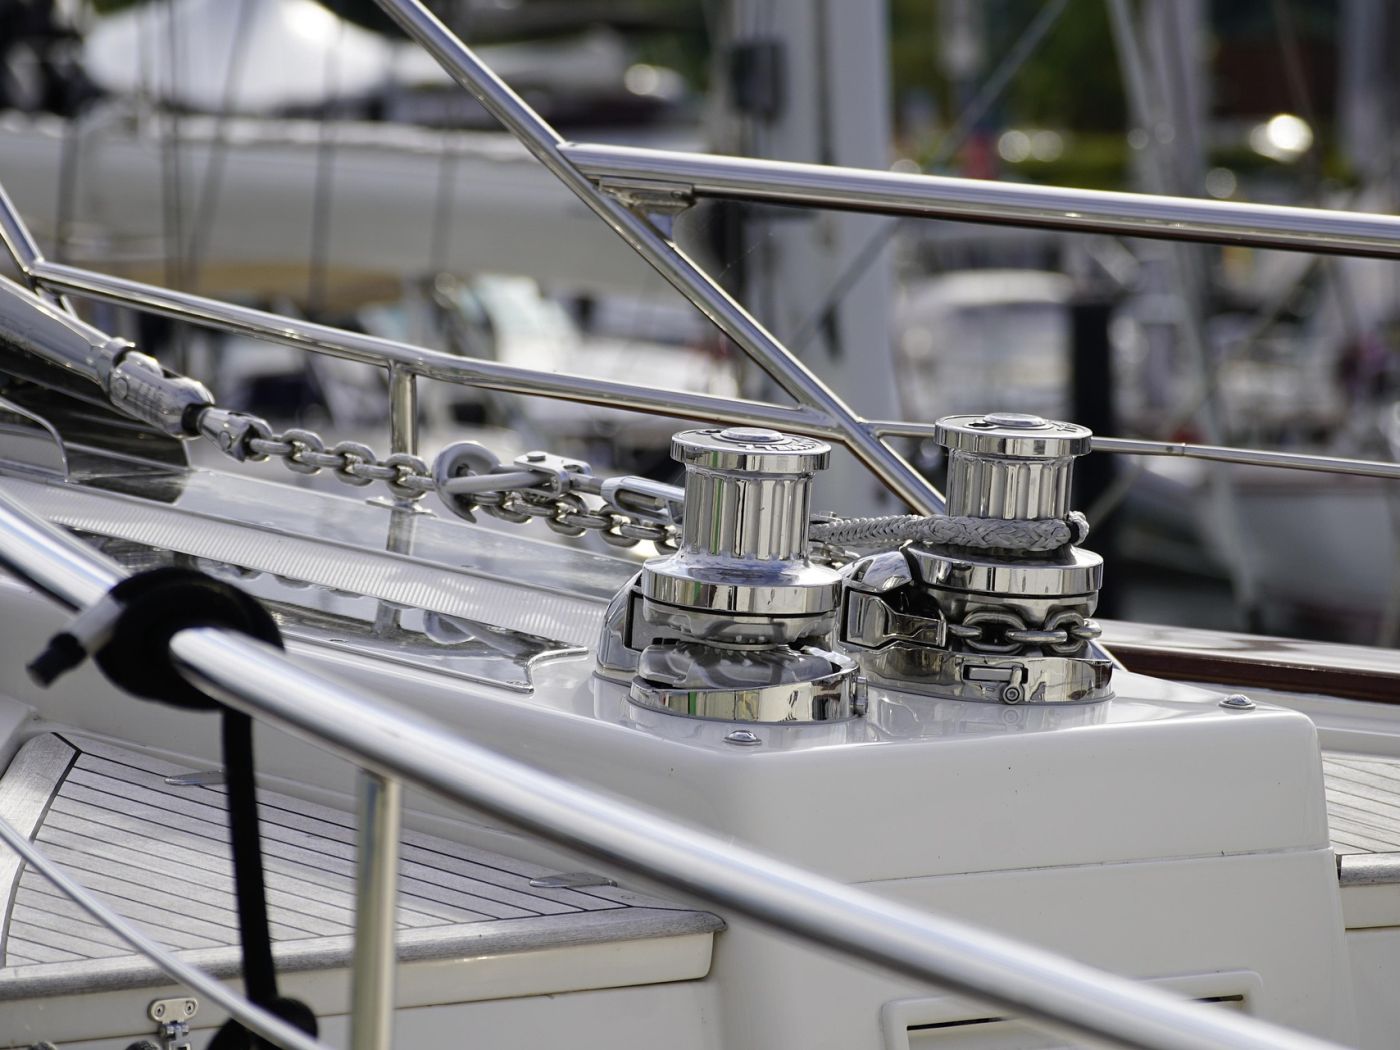
Two coils of short-link anchor chain can carry the same 10 mm stamp and still behave differently on the same windlass. One length drops into the gypsy pocket and pays out smoothly; the other sits a little high on the tooth tips, and under load it starts to skip — one link riding up, the next landing hard, the chain climbing across the sprocket instead of seating in it.
The diameter stamp is not wrong. A 10 mm chain does have a nominal bar diameter of about 10 mm. What the stamp does not tell you is the length of each link or the width of the opening inside it, and those are the dimensions a windlass sprocket actually grips. Two chains can share a nominal diameter and still differ enough, link by link, that one fits a pocket cut for a different calibration and the other does not.
For anyone replacing a rode or specifying a new one, that turns a simple measurement into a short sequence of questions: which calibration the chain is made to, what the finished link measures, and what the gypsy on the windlass was cut for. This article works through those three in order.
2. What Each Link Dimension Actually Measures
Before any chart is useful, it helps to fix what each dimension means, because the same link is described with different symbols in different documents.
- Bar (wire) diameter — d. The thickness of the steel forming the link. This is the "nominal size" printed on the label: 6 mm, 8 mm, 10 mm.
- Pitch — p. The inside length of a single link, measured between the inner faces at the ends of the link. Some documents call it the internal length.
- Internal width. The clear opening between the two sides of a link.
- External width. The outside width of a link, measured from outer edge to outer edge.
A distinction matters here as much as the definitions: a nominal marking, a measured dimension, and a limit dimension are three different things. The nominal size is a label. The measured dimension is what a caliper reads on a specific piece of chain. The limit dimension — a specified minimum or maximum — is what a standard permits, and it is the one to compare against when deciding whether a chain will seat.
The two metric standards used in this article label the same geometry differently. DIN 766 uses d for the bar diameter, t for the internal length (pitch), b1 for the internal width, and b2 for the external width. ISO 4565 uses dn for nominal diameter, p1 for pitch, w1 for internal width, and w for external width, stating w1 as a minimum and w as a maximum.
d (DIN 766) | dn (ISO 4565)
thickness of the round steel — "10 mm" chain is 10 mm wire
t (DIN 766) | p1 (ISO 4565)
clear length inside one link
b1 (DIN 766) | w1 min (ISO 4565)
clear opening inside the link
b2 (DIN 766) | w max (ISO 4565)
outer edge to outer edge
| Dimension | What it measures | DIN 766 | ISO 4565 |
|---|---|---|---|
| Bar (wire) diameter | Thickness of the round steel the link is bent from — the nominal size on the label, for example 10 mm | d | dn |
| Internal length (pitch) | Clear distance inside the link, from the inner edge of one end to the inner edge of the other | t | p1 |
| Internal width | Clear width of the opening inside the link | b1 | w1 (stated as a minimum) |
| External width | Outside width across the link, from outer edge to outer edge | b2 | w (stated as a maximum) |
3. Two Metric Calibrations: DIN 766 and ISO 4565
Short-link anchor chain for small craft is calibrated under two separate metric families, and the difference between them is not cosmetic.
ISO 4565:1986 applies to anchor chains of nominal diameter 6 mm to 12 mm for small craft, controlled by the craft's windlass; the standard states that it does not apply to chains used for lifting. Its dimensions follow a simple basis: pitch p1 is three times the nominal diameter dn; the minimum internal width w1 is 1.35 times dn; and the maximum external width w is 3.6 times dn. Those relationships produce the ISO rows in the chart below.
DIN 766 is a separate metric short-link chain standard that tabulates a wider set of nominal sizes. It is not a translation of ISO 4565, and the two are not interchangeable. A length of chain is made, marked, and supplied to one calibration family, not to both at once.
Nowhere is that clearer than at 10 mm, the one common size where the two families part company on pitch: DIN 766 specifies 28 mm and ISO 4565 specifies 30 mm for the same nominal bar diameter. At 8 mm the pitch happens to coincide at 24 mm in both, yet the permitted maximum external width still differs — 27.2 mm under DIN 766 against 28.8 mm under ISO 4565. The two calibrations are distinguished by the whole set of link dimensions, not by a single size or a single number.
4. Anchor Chain Size Chart (Identification Reference)
The table below lists link geometry as published by each standard, at the nominal sizes where those values are available. It is included so a buyer can identify what a chain is likely to be — not to approve a gypsy fit.
| Spec series | Nominal chain dia. d (mm) | Pitch / inside length (mm) | Inside width (mm), ISO w1 min / DIN b1 | Outside width (mm), max — ISO w max / DIN b2 max |
|---|---|---|---|---|
| ISO 4565 | 6 | 18 | 8.1 | 21.6 |
| ISO 4565 | 8 | 24 | 10.8 | 28.8 |
| ISO 4565 | 10 | 30 | 13.5 | 36 |
| ISO 4565 | 12 | 36 | 16.2 | 43.2 |
| DIN 766 | 6 | 18.5 | 7.2 | 20.4 |
| DIN 766 | 7 | 22 | 8.4 | 23.8 |
| DIN 766 | 8 | 24 | 9.6 | 27.2 |
| DIN 766 | 10 | 28 | 12 | 36 |
| DIN 766 | 11 | 31 | 13.2 | 40 |
| DIN 766 | 13 | 36 | 15.6 | 47 |
| DIN 766 | 14 | 41 | 16.8 | 50 |
| DIN 766 | 16 | 45 | 19.2 | 58 |
Purpose and source of the chart. This chart is an identification reference, not a gypsy compatibility approval. The ISO 4565 values are taken from the dimension table of the standard itself; the DIN 766 values are transcribed from the standard's table through an industry reference and cross-checked against a chain manufacturer's technical data. No manufacturer-specific approximation is included, and no cell is filled by extrapolation from a neighbouring size. The figures are the standards' own limits: ISO internal width as a minimum, ISO external width as a maximum, and DIN 766 external width b2 as a maximum, with DIN 766 internal width b1 tabulated as the internal width.
The two 10 mm rows are the pair most often confused in the field. Their pitch differs by 2 mm per link, and across a length of chain that difference accumulates — which is why a mismatched calibration tends to show up as skipping rather than as an obviously wrong chain. Measuring several links in series, rather than a single link, is the practical way to see which calibration a chain is made to.
5. Why the Gypsy, Not the Label, Decides Fit
A windlass gypsy — the chainwheel — is not a general-purpose sprocket. Its pocket is machined to accept a specific link: a particular bar diameter, a particular pitch, and a particular width. All three are cut into the same pocket, so a chain has to satisfy all three at once, not merely the nominal diameter.
The mechanism is easiest to see in pitch. As the chain runs, each link has to drop into a pocket and lie flat against its seat while the following link is picked up by the tooth. If the pitch is too long for the pocket, the link lands on the tip of the tooth instead of the seat. Under tension the chain rides up, the next link mis-seats as well, and the run becomes a series of skips — the chain climbing across the sprocket rather than gripping it. If the pitch is too short, links crowd the pocket and the chain binds. Width faults behave the same way on the other axis: a link too wide bridges the pocket walls and cannot seat, while a link too narrow moves loosely and can twist instead of tracking.
This is also why a bench test proves very little. Dropping a few links into a gypsy by hand, or turning the chainwheel slowly with no load, can look convincing on a chain that will misbehave once tension and motion are applied. The pocket only has to accept every link, over a full run, under the load of retrieval. A working margin is built into the pocket by the windlass maker, but the size of that margin varies between models, and no single tolerance figure applies to every gypsy.
The practical conclusion is that the gypsy's own marking is the primary identifier. The stamping on the chainwheel, read together with the windlass manual, names the standard and the size the pocket was cut for. Chain must not be run on a gypsy machined for a different standard, even when the nominal size looks the same.
6. A Procurement Check Order
For a replacement rode or a new build, the checks run in this order — from the fixed part of the system to the variable part:
- Read the gypsy first. Identify the windlass and chainwheel model, and read the stamping on the gypsy together with the windlass manual. The marking names the standard and nominal size the pocket was cut for; it is the fixed reference for everything that follows.
- Match the chain's declared standard and marking. Confirm which calibration family the chain is made to and what the maker marks it as, and check that this corresponds to the gypsy.
- Verify the finished dimensions against a sample. Lay at least ten links flat, pull them tight, and measure from outside edge to outside edge on a clean, unworn section; a single link is impractical to measure accurately. Compare the result against the maker's declared dimensions for that calibration. A worn chain will measure longer than it was made, so a used chain must not be the sole basis for sizing a new one.
- Get the exact specification in writing and run the specified fit check. Confirm the supply specification with the chain maker and the windlass maker, and carry out the fit check the windlass maker specifies before committing a full length to the vessel.
Steps one and two establish which chain is even a candidate. Steps three and four confirm that the chain actually delivered matches — and they are the steps most often skipped when a replacement is ordered against a diameter alone.
7. What to Send Us
Fit confirmation is a documentation exercise before it is a purchase. To confirm the exact supply specification for a chain on a given windlass, send us:
- the windlass and gypsy model, or the stamping on the chainwheel;
- the marking on the chain currently in use (standard and size);
- the chain specification required — calibration family, nominal size, and required length;
- any relevant drawing or windlass manual page.
We will work from those to confirm the specification of what we can supply. We do not certify a gypsy-and-chain combination from a single dimension, and we cannot promise that an arbitrary chain and gypsy will be compatible — that depends on the calibration and the manufacturing tolerance of the gypsy, both of which the windlass maker controls.
Our current anchoring hardware is listed under anchor chain. Where a stainless steel DIN 766 chain entry is relevant, it is listed here: stainless steel DIN 766 anchor chain. That product listing is an entry point only; it is not by itself evidence that a given batch conforms to any particular standard, and dimensional confirmation still comes from the maker's documentation.