At Andy Marine, we believe that practical manufacturing knowledge is one of the most valuable assets built over time.
Inside our workshop, there are engineers, production specialists, and experienced technicians who have spent years working with stainless steel marine hardware — from material selection and casting processes to finishing and quality control.
Many of these insights are learned through daily production experience: understanding why a component fails, how different materials perform in marine environments, and what details truly matter when developing reliable hardware.
However, this practical knowledge is often shared only within the workshop and rarely reaches customers who are making sourcing and engineering decisions.
ENGINEER TALKS is our effort to organize these conversations and share the manufacturing experience behind marine hardware.
Through this series, we discuss materials, production processes, design considerations, and real-world lessons from the perspective of a marine hardware manufacturer.
Today's ENGINEER TALKS Ep.24 is presented by Engineer Li, written by me the editor.
Brown Marks on 316 Are a Symptom, Not a Verdict
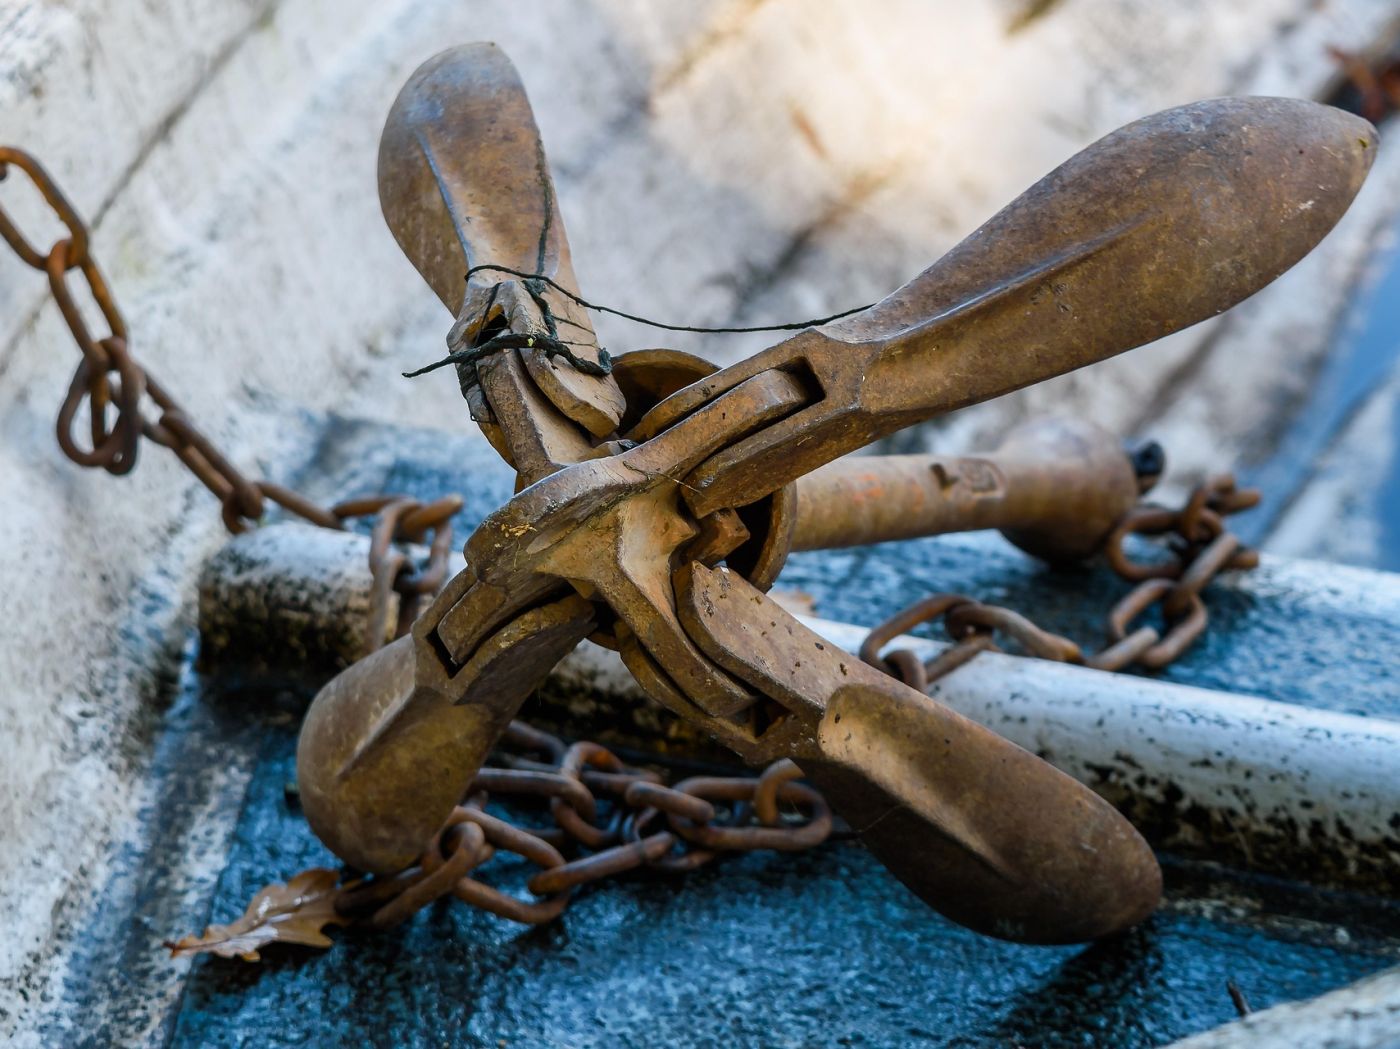
Every few seasons, a yard or a distributor opens a crate of 316 stainless deck hardware and finds tea-coloured streaks, a scatter of rust freckles, or a weeping rust line running out from under a baseplate. The first question is almost always the same: is this the wrong grade, or a bad batch?
The colour of the mark, on its own, answers very little. Brown discolouration on 316 can come from at least four different situations, and they do not carry the same meaning:
- Atmospheric tea staining — a thin surface discolouration that forms on stainless steel in coastal, industrial or urban air. In the industry literature it is described as a cosmetic condition of the surface rather than a loss of structural integrity or service life, and that description is written for atmospheric exposure.
- Foreign iron contamination — particles of ordinary or low-alloy steel that landed on the surface, or were pressed into it by a wire brush, grinding wheel or lifting sling, and are now rusting in their own right.
- Pitting — a localised breakdown of the passive film on an openly exposed surface.
- Crevice corrosion — attack that develops inside a tight joint, under a fastener head or beneath a deposit, where the local chemistry has changed.
These conditions are not mutually exclusive. A part that has been sitting wet in a sheltered corner with a smear of steel dust on it can show tea staining, embedded-iron freckles and the start of pitting at the same time. That is why a photograph cannot be read like a label. The purpose of an inspection is to separate two very different statements: something is sitting on the surface, or the base metal is being consumed.
Grade 316 earns its place in marine hardware because its molybdenum content — on the order of 2–3% — raises its resistance to chloride pitting and crevice attack relative to lower-alloyed stainless grades. That advantage is real, and it is also why a brown mark on 316 deserves to be read carefully rather than waved away. It is not a licence to use 316 in every marine exposure. Marine-industry guidance generally positions 316 for hull and deck fittings above the waterline, and treats immersed service where tight crevices exist as the condition in which it is most likely to be the wrong choice.
Record First, Clean Second
If the first thing you do to a stained part is grind, sand or heavy-buff it to "see what is underneath," you will usually destroy the evidence you need and may leave a fresh, disturbed surface behind. The order matters: record, then clean, then look.
Before any cleaning, capture:
- Position and orientation — where the part sits on the vessel, whether it faces the weather or is sheltered, and whether water stands on it or drains away.
- Exposure — distance from the water, splash zone versus immersed, and whether the area stays wet between wash-downs.
- Recent work nearby — carbon steel cutting, grinding or welding; wire brushing; galvanised fittings; or acid and bleach cleaning of surrounding surfaces.
- Maintenance history — when the part was last washed and with what.
- Images — dated photographs with a scale reference, and close-ups showing whether the mark is a flat film or a depression.
Only then clean, and use the gentlest method that will reveal the substrate. Industry guidance for stainless steel recommends washing with soap or a mild detergent and warm water, followed by a clean cold-water rinse and a wipe dry. Abrasive cleaners and cleaners that contain chlorides or bleach should be avoided, and hydrochloric acid — sometimes reached for to strip cement or mortar residue — should not be used on stainless steel at all. The point of cleaning at this stage is to remove deposits and expose the underlying surface, not to remove metal.
Two things are worth stating plainly here. Cleaning reveals; it does not repair, and it does not bring back metal that has already been lost. And a freshly cleaned surface is not automatically a corrosion-resistant one until its passive film has had a chance to reform in air.
Reading the Part: Four Checkpoints
Walk the inspection in a fixed order so that the same observations are recorded every time, whoever is doing the work.
1. Where is the mark? Location is often the single most useful clue. Rust that follows a water path from a carbon steel fitting above points toward contamination carried by runoff. Marks concentrated under a fastener head, inside a hinge knuckle, beneath a sealant line or under marine growth point toward a crevice. Isolated freckles scattered across an open, exposed face behave differently again.
2. What is sitting on the surface? Before cleaning, note whether the mark is a flat discolouration, a raised deposit, or a distinct pit. Then clean and rinse as above and re-examine. Discolouration that washes off leaves a sound surface behind; a genuine pit does not disappear. Where free iron is suspected, a ferroxyl test — the potassium ferricyanide test recognised in the ASTM A380 cleaning and passivation practice — or a simple water mist-and-dry cycle can act as a screening step after cleaning. It is worth remembering that visual inspection is good at finding gross contamination but can miss thin films and transparent residues.
3. What does the substrate look like after cleaning? This is the step that separates the categories. A clean surface with no pitting, no dishing and no roughness is consistent with surface staining or removable contamination. A surface that still shows discrete pits, or a shallow depression with a rough floor, has lost metal, and that is a different conversation. Crevice corrosion is especially easy to miss, because it can be well advanced inside a joint while the exposed face around it looks clean.
4. Does it come back? Recurrence is diagnostic. A stain that stays gone after a proper wash behaves like an external deposit or an atmospherically driven film. Rust that returns quickly at the same spot, or that keeps weeping from the same joint, suggests an ongoing source — a contamination reservoir, a pocket that never drains, or a crevice that is still starved of oxygen.
Inspection Clues at a Glance
| What you see | Check first | What it does not prove | Next step |
|---|---|---|---|
| Flat, uniform browning over a sheltered or splash-wet face | How the part drains and whether the area stays wet | That the grade is wrong, or that the part is structurally compromised | Record conditions, then wash with mild detergent and rinse; re-inspect the substrate |
| Rust freckles near recent steel work, or following a water path | Nearby carbon steel cutting, grinding, welding, wire brushing or runoff | That the mark comes from the hardware itself | Clean; screen for free iron by ferroxyl test or mist-and-dry; remove the contamination source |
| Marks concentrated under a head, gasket, sealant line or marine growth | Whether the joint holds water and excludes oxygen | Anything about the exposed face elsewhere on the part | Inspect the crevice itself; treat as a potential crevice-corrosion site if pits are found |
| Discrete pits or dished depressions that survive cleaning | The depth and extent of metal loss, and whether the part is load- or safety-critical | That pits are acceptable at some standard depth | Stop treating as cosmetic; refer to a qualified engineer for assessment |
| Rust that returns quickly after cleaning at the same spot | An ongoing contamination source or an undrained pocket | That the cleaning was done incorrectly | Find and remove the source; re-evaluate drainage and the joint design |
Why It Happens: Three Mechanisms Behind the Marks
Underneath the categories, three mechanisms explain most of what a yard actually sees.
Salt deposition and moisture. Sea salt is hygroscopic: it pulls moisture out of the air and holds a wet film on a surface at humidities where clean water alone would evaporate. That film is a chloride-bearing electrolyte sitting on the metal, and where it persists — a sheltered face that rarely sees rain, a horizontal ledge, a surface that is never rinsed — it is enough to discolour the surface. This is the mechanism behind atmospheric tea staining, and it is a surface phenomenon.
Foreign iron. When particles of ordinary or low-alloy steel are left on a stainless surface, or are pressed into it by a wire brush, a grinding wheel or a lifting sling, they rust under conditions where the stainless around them does not. The rust deposit holds moisture against the steel and creates exactly the kind of local, oxygen-restricted environment in which localised attack can begin. What looks like the hardware rusting may in fact be the contaminant rusting on top of it.
Oxygen-restricted crevices. Inside a tight joint — under a fastener head, between clamped faces, beneath a gasket or a patch of marine growth — the oxygen in the trapped water is consumed faster than it can be replaced. The crevice becomes oxygen-depleted, chloride-enriched and slightly acidified, and the passive film can break down while the open surface right beside it stays clean. This is the mechanism that makes crevices the practical limit for 316 in immersed service, and it is why a component can show no pitting at all on its exposed faces and still be corroding inside a joint.
It would be too simple to say that stainless steel only corrodes where there is no oxygen. The passive film needs oxygen to repair itself, but localised attack depends on the whole local chemistry — chloride concentration, temperature, acidity and how well the surface drains — not on the absence of oxygen alone.
When to Stop Treating It as a Cosmetic Issue
Not every brown mark needs a procedure, and not every one can be handled with a cloth. A reasonable split:
- Surface staining or removable contamination — where cleaning removes the mark and the substrate underneath is sound, treat it as a maintenance matter. Wash, rinse, dry, and correct whatever let the deposit build up: improve drainage, remove the contamination source, and set a realistic cleaning interval.
- Confirmed or suspected free iron — remove the source of the contamination, then have the surface treated so that the passive film can re-form properly. Passivation is aimed at removing exogenous free iron; it is not a substitute for cleaning, it does not remove embedded particles or heat-tint scale, and it cannot be applied successfully to a surface that is still contaminated.
- Pitting, crevice corrosion, or any suspected loss of section — stop treating the part as a cosmetic problem. Once metal has been consumed, particularly in a crevice, along a crack, or at a load-bearing or safety-critical connection, the question shifts from appearance to fitness for purpose. That assessment belongs to a qualified engineer, using the manufacturer's guidance and, where relevant, non-destructive inspection. There is no universal "acceptable pit depth" that an article can hand out for real hardware.
Where deeper treatment is required — pickling, passivation or electrochemical cleaning — it should be carried out by a qualified surface-treatment provider working to an applicable standard. The two documents most often referenced as the treatment framework are the ASTM A380 practice for cleaning, descaling and passivation of stainless steel parts, which also lists methods for detecting free iron, and the ASTM A967 specification for chemical passivation treatments. This article deliberately does not provide acid concentrations, temperatures, immersion times or mixing instructions; those are process variables that belong with the treatment provider and the applicable standard, not with a yard mixing chemicals on a dock.
What to Specify Before It Ships
Most brown-mark disputes are settled long before anything reaches the water — in what the purchase order did and did not say. Buyers who want to avoid the argument should put these items on the specification:
- Grade and evidence — the exact grade required, and the material certificates or mill certificates that should accompany it, with a chemistry that can be checked against the specified grade.
- Surface treatment — whether the surface is to be supplied to a defined finish, and whether any passivation or other surface treatment is required, and how it is to be verified.
- Drainage and crevice detail — baseplates and covers that drain rather than trap water, and an explicit look at where tight joints, blind fasteners or gasket lines could create a crevice.
- Packaging and handling — control of iron contamination during machining, finishing, packing and transport; no carbon steel wire brushing; protection that keeps steel dust and swarf away from finished surfaces.
- Inspection and acceptance — the inspection method and the acceptance criteria agreed up front, so that "is this acceptable?" has a defined answer rather than an opinion.
These are buyer-side clauses, not statements about any particular supplier. The point is that grade, surface condition and cleanliness can all be specified and verified; leaving them implied is what turns a normal maintenance question into a warranty argument.
Discussing Material and Surface Requirements
If you are specifying or sourcing stainless marine hardware and want to work through what a given exposure — atmospheric, splash zone or immersed — actually requires in terms of grade, surface condition and inspection criteria, send us the component location, the service environment, and photographs or drawings of the part. We can discuss material and surface requirements against your application and help you set acceptance criteria that hold up at handover.